
Food Industry Metal Detectors: Principles Of Operation And Key Components

Food industry metal detectors are electronic systems designed to identify metallic contaminants within food and food packaging during processing. They typically operate by generating an alternating electromagnetic field and monitoring changes in that field caused by metal objects passing through a sensing aperture. Key components include a transmitter coil that produces the field, receiver coils or sensors that detect field disturbances, a control unit with signal processing algorithms, and a physical or pneumatic rejection device that removes detected contaminants from the product stream. These systems are often integrated into conveyors, free-fall chutes, or pipelines according to product form.
Detection performance in food production depends on several interacting factors: the electromagnetic design of the detector, the type and geometry of the contaminant, the product’s electrical and magnetic properties, and the packaging material. Systems may be configured to detect ferrous, non-ferrous and certain grades of stainless steel, though sensitivity to particular metals can vary. Placement, aperture size, conveyor speed and environmental electrical noise are further practical considerations. Operators often balance sensitivity and false-reject rates to align with hygiene requirements and inspection protocols.
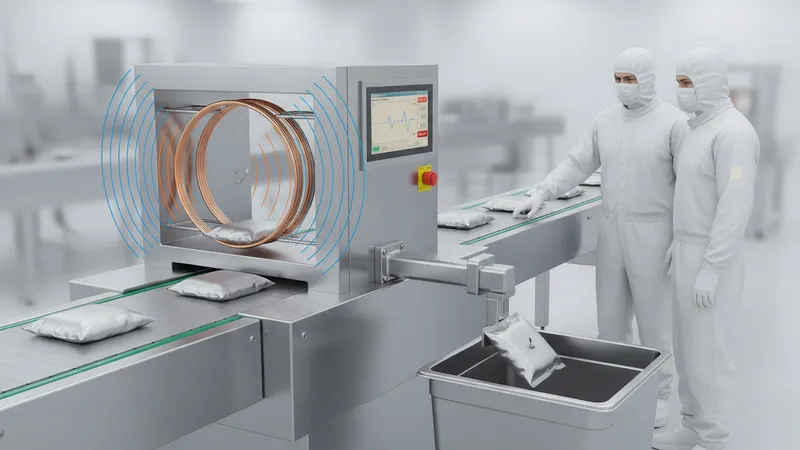
- Conveyor-based in-line metal detector systems — Continuous aperture units mounted over conveyor belts for packaged or bulk products; typically combined with automatic reject mechanisms and variable aperture sizes to match product dimensions.
- Pipeline or in-line detectors for pumped or liquid products — Circular or oval apertures designed to surround a sanitary pipe section, enabling inspection of liquids, pastes and slurries with minimal flow interruption.
- Portable and handheld detectors for spot checks — Compact units used for manual inspection of raw ingredients, finished packs, or equipment surfaces to supplement fixed-line inspection regimes.
Electromagnetic principles underlie practical detector designs. A transmitter coil creates an alternating magnetic field; a conductive or ferromagnetic object disturbs that field and induces a secondary response that receiver coils detect. Balanced coil arrangements and digital signal processing may reduce background interference and improve stability. Modern units often include multi-frequency operation to improve detection of different metal types. Environmental sources of electromagnetic interference, such as motors or drive inverters near the line, can affect signal stability and therefore require mitigation through grounding, shielding, or site layout adjustments.
Material response varies by metal type and geometry. Ferrous metals typically produce a strong magnetic response and may be easier to detect at smaller sizes, while non-ferrous metals such as aluminum induce weaker distortions that can require higher sensitivity or multi-frequency detection. Austenitic stainless steels are often more challenging because they are less magnetic and may only be detectable when corrosion, inclusions, or conductive properties provide a sufficient signal. Many suppliers and standards reference sensitivity in terms of the diameter of a spherical test-piece of defined metal at the aperture centre; this provides a comparative measure but may not reflect every real-world shape.
Product and packaging characteristics frequently influence detection limits. High-moisture, high-salt, or conductive products can create a product effect that masks metal signals; similarly, metallic packaging or foil can create background signals that need compensation. Conveyor and pipeline integration are designed to minimise product effect by controlling orientation, spacing and speed. Free-fall or chute applications may require special apertures to reduce motion-related signal variability. Hygiene and sanitary design of detectors and associated conveyors or pipe sections is often mandated in processing environments to facilitate cleaning and reduce contamination risks.
Rejection mechanisms and operational testing form part of a defensible inspection strategy. Common reject types include pneumatically actuated air-blasts, mechanical pushers, diverter gates, and hold-and-inspect pockets. Regular testing with calibrated test pieces is typically used to confirm ongoing sensitivity and to document system performance as part of quality control records. Maintenance, firmware updates, and periodic recalibration may also be planned to maintain consistent detection performance over time. The next sections examine practical components and considerations in more detail.